

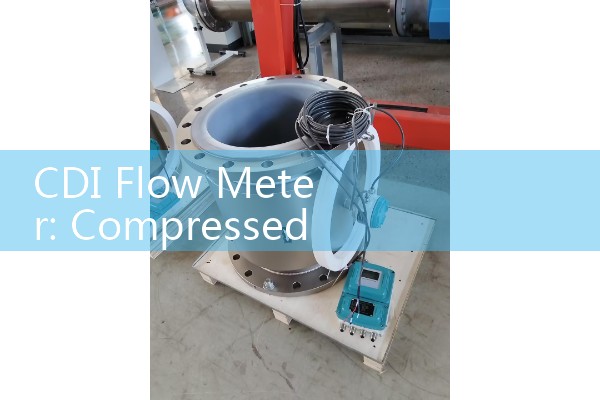
『CDI Flow Meter: Compressed Air System Energy Auditing Equipment』Related information(flow rotameter|digital flow meter|balo meter|hydraulic flow meter|volumetric meter|positive displacement meter|pitot tube flow meter|displacement meter|cfm meter|variable area flow meter|inline flow meter|differential pressure flow meter|calibrated flow meter|velocity meter|paddle wheel flow meter|oval gear flow meter|anemometer hvac|multiphase flow meter|doppler flow meter|thorpe tube flowmeter|heat flow meter)
CDI Flow Meter for Compressed Air System Energy Auditing: What You Actually Need to Know
Quick Answer: A CDI flow meter is a thermal mass flow meter built specifically for compressed air and gas auditing. It installs directly into compressed air lines and measures mass flow, temperature, and pressure in real time. Most plants lose 20 to 30 percent of compressed air to leaks. A proper audit tool like this pays for itself within 3 to 6 months.
Silver Automation Instruments deals with industrial flow measurement day in and day out. One of the most common calls we get comes from plant engineers who just received a shocking energy bill. They know compressed air is expensive. They do not know where the waste is hiding. A CDI flow meter or an equivalent thermal mass flow meter gives them the answer inside the first hour of logging.
We work with customers across Southeast Asia, the Middle East, and Africa. A food packaging plant in Ho Chi Minh City called us last year. Their compressor ran 24/7. They thought everything was normal. We recommended a thermal mass flow meter for compressed air auditing with data logging capability. Within two weeks they found leaks costing them 14,000 USD per year. That is a real number from a real site.
What a CDI Flow Meter Does Inside a Compressed Air Line
A CDI style flow meter uses the thermal dispersion principle. Two PT100 RTD sensors sit inside the pipe. One sensor measures the gas temperature. The other heats up to a set point above that temperature. As gas flows past the heated sensor, it cools down. The meter calculates mass flow based on how much energy it takes to maintain the temperature difference. No external temperature or pressure compensation is needed. The meter outputs mass flow directly in kg/h or SCFM.
This matters because compressed air changes density with pressure and temperature. A volumetric flow meter like a vortex meter will give you readings that shift with operating conditions. A thermal mass flow meter gives you the actual mass of air moving through the pipe. For energy auditing, mass flow is the number you need.
Most CDI type meters come with a built-in display showing flow rate, totalized flow, and temperature. Some models include a pressure sensor too. The output is almost always 4-20 mA, pulse, or RS485 Modbus RTU. Many auditors connect the meter to a laptop via USB and run logging software for 7 to 30 days. The data reveals usage patterns, peak demand times, and leakage rates during shutdown periods.
Why Compressed Air Audits Always Start with Flow Measurement
Compressed air is one of the most expensive utilities in a factory. Producing one cubic meter of compressed air at 7 bar costs roughly 7 to 10 times more than the equivalent electricity. The problem is that most plants have no sub-metering on their compressed air system. They see the total electricity bill. They cannot see which department, which shift, or which machine is wasting air.
A compressed air flow meter for energy audits changes that picture instantly. You clamp it onto the main header or branch lines. You let it log for a week. Then you pull the data and look at the flow during non-production hours. If flow is non-zero when the plant is shut down, you have leaks. It really is that simple.
One of our distributors in Dubai did this for a plastics injection molding facility. The plant manager believed his system was tight. The audit showed 35 percent of total air production was disappearing through leaks and open blow-offs during weekend shutdowns. They fixed the leaks and saved enough to buy two new compressors over three years.
System pressure also drops when leaks exist. Operators compensate by raising the compressor set point. Every 1 bar increase in system pressure adds about 7 percent to energy consumption. So leaks trigger a chain reaction of higher pressure settings and even more waste. A flow meter audit breaks that cycle.
Thermal Mass Flow Meter Specifications That Matter for Auditing
When you select a flow meter for compressed air auditing, focus on these parameters. Pipe size is the starting point. Thermal mass flow meters work well from DN15 up to DN300 and beyond. For insertion probes, you need a 1/2 inch or 3/4 inch ball valve hot tap fitting. Inline meters with flanged or threaded connections suit smaller lines.
Turndown ratio is critical for audit work. You need a meter that can measure from near zero flow during shutdown up to peak demand during full production. Look for a turndown of at least 100:1. Some thermal meters go to 1000:1. This wide range lets you catch small leaks that a vortex or orifice plate meter would miss entirely.
Accuracy for a good thermal mass flow meter sits at plus or minus 1 to 1.5 percent of reading above 50 percent of full scale. Below that, most manufacturers quote plus or minus 0.5 percent of full scale. For audit purposes, repeatability matters more than absolute accuracy. You are comparing before and after measurements on the same meter. A repeatability of plus or minus 0.2 percent is achievable
Response time is another factor. A fast response sensor catches transient events like a stuck blow-off valve opening. Look for a response time under 1 second for the flow signal. Temperature compensation should be built in and automatic.
Power options include 24 VDC loop-powered models for simple 4-20 mA output, or 85-265 VAC powered units with full Modbus and display capabilities. For field audits, a USB powered data logger combined with a loop-powered meter is the lightest setup. For permanent monitoring, AC powered meters with RS485 and Ethernet ports feed data directly into plant SCADA systems.
Silver Instruments Thermal Mass Flow Meter for Audit Applications
Silver Automation Instruments supplies thermal mass flow meters designed for compressed air, nitrogen, CO2, argon, and natural gas measurement. Our meters use the same thermal dispersion principle found in CDI type audit devices. Dual PT100 sensors handle gas temperatures from -40 to 300 degrees Celsius. Pressure ratings go to 40 bar standard, with higher ratings available on request.
We offer both inline and insertion configurations. Inline meters cover DN15 to DN80 with threaded or flanged connections. Insertion probes cover DN80 to DN300 and larger. The insertion version installs through a 1 inch ball valve, so you can mount and remove the probe without shutting down the air supply. This is exactly what field auditors need when they move from one measurement point to another.
The built-in display shows mass flow rate in kg/h or Nm3/h, totalized flow, and gas temperature. Output options include 4-20 mA, pulse, and RS485 with Modbus RTU protocol. Data logging is straightforward. Connect the RS485 output to a USB adapter. Run the free logging software on a laptop. Set the sampling interval to anywhere from 1 second to 1 hour. Export the data as CSV for analysis in Excel.
Most of our customers operate in regions with challenging conditions. High humidity in Southeast Asia. Dusty environments in the Middle East. Unstable power in parts of Africa. Our meters ship with IP66 or IP67 rated enclosures. The sensor elements are protected against moisture ingress. We have units running in a palm oil refinery in Indonesia, a cement plant in Nigeria, and a beverage bottling line in Peru. All of them measure compressed air flow continuously for both energy management and process control.
Installation Tips That Prevent Measurement Errors
Most engineers skip the installation details and then wonder why readings drift. Here is the thing. Thermal mass flow meters need straight pipe upstream and downstream of the sensor. Ten diameters upstream and five diameters downstream is the standard rule. If you have a valve, elbow, or tee within that distance, add a flow straightener or increase the straight run.
Moisture is the biggest enemy of a thermal sensor. Compressed air always contains some water vapor, even after drying. Install the meter after the dryer and after the filter. If the sensor tip collects water droplets, the cooling effect on the heated RTD creates false high flow readings. We have seen this on customer sites many times. A simple coalescing filter upstream solves the problem.
Mount the probe so the sensor tip reaches the center of the pipe. Flow velocity is highest at the center. Placing the sensor at the pipe wall or in a stagnant zone will under-report flow by 20 to 40 percent. Most insertion probes have depth markings on the stem. Use them. Do not guess.
For compressed air at pressures above 10 bar, confirm the meter calibration covers your operating pressure. Some manufacturers calibrate at atmospheric pressure only. A meter calibrated at 1 bar will read wrong at 10 bar if the calibration does not compensate for the thermal conductivity change of the gas. Always specify your operating pressure when ordering. Silver Instruments calibrates at your actual working pressure or provides a pressure correction curve.
Data Analysis: What the Numbers Tell You
Raw flow data from a logging session contains more insights than most people realize. The first thing you check is the baseline flow during non-production hours. Anything above zero is a leak. Multiply that flow rate by the number of non-production hours per year. Multiply by your cost per cubic meter of compressed air. That number is your annual leak cost.
The second layer of analysis looks at flow patterns during production. Compare flow to the production schedule. If flow stays high even when machines are idle, operators may be leaving air tools connected or blow-off nozzles open. Training fixes that. Equipment does not need to change.
The third layer is pressure versus flow. If flow demand spikes periodically and pressure dips at the same time, your compressor may be undersized or your storage receiver may be too small. A pressure dip of 0.5 bar during peak demand tells you to add receiver volume or look at the compressor sequencing.
A textile mill in Bangladesh logged data for 14 days using a Silver Instruments thermal mass flow meter. They identified a pressure drop of 0.8 bar bet
 Hot Blog
 Related AD